shining bright

a British lighting manufacturer with a difference

Obsessed with solving problems, not just selling 'stuff': we were born from a belief that the lighting industry deserved better.

What Are the Top Types of Glass Sorting Machines?

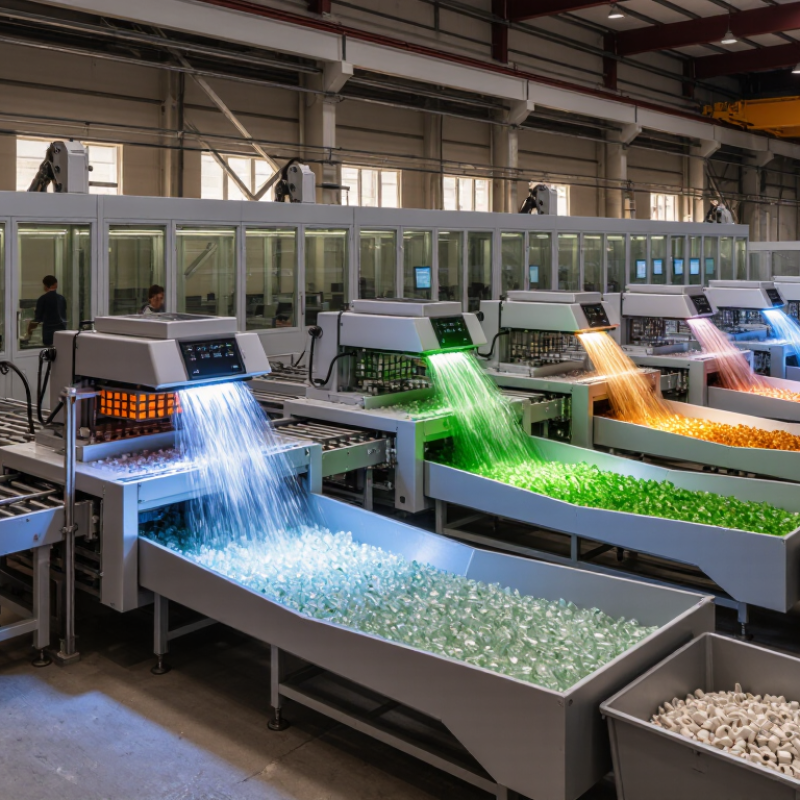
Glass recycling begins with a deceptively simple question: what should stay, and what must leave? A Glass Sorting Machine answers by identifying color, material, or unwanted pieces as glass moves along a belt. Clear, green, and amber fragments may need separate routes. A small ceramic shard can matter, too. One missed contaminant may affect an entire batch.

The main machine types include color sorters, optical contaminant sorters, and systems designed to remove ceramics, stones, and porcelain. Some combine cameras, sensors, and air jets; others use different detection methods for specific feedstocks. The right choice depends on fragment size, incoming contamination, throughput, and the quality target. Conditions matter. Dust, broken labels, and uneven lighting can complicate detection, so machine specifications alone do not tell the whole story.

This introduction uses an illustrative expert voice, not a verified interview quotation. Glass-recycling process engineer “Alex Morgan” offers this guiding line: “A sorter performs best when the feed is consistent and the target is clear.” Treat that as an editorial principle, not a sourced statement. The guide ahead compares the leading machine types, explains what each detects, and points out practical trade-offs. No single setup fits every plant. Real-world trials still matter.
What Are the Top Types of Glass Sorting Machines?

Mechanical Systems for the Initial Separation of Glass

Mechanical systems make the first cut in glass sorting. Vibrating screens separate fines from larger cullet, while trommel screens rotate mixed material through perforated drums. Their openings determine which fragments pass through. Set them too small, and useful glass may leave with the fines. Set them too large, and ceramics or caps can travel downstream.

Magnets remove ferrous pieces before optical inspection; air classifiers can lift light labels and film. These steps reduce the burden on later equipment, but they do not guarantee clean cullet. Small details matter. A wet feed or worn screen can shift separation quality, so operators should check screen condition and sample output regularly. Eurostat’s Packaging Waste Statistics report a 75.9% recycling rate for glass packaging waste in the EU in 2022. That figure describes the broader recycling system, not any single machine’s performance. Mechanical separation is only one stage, and its results depend on the incoming material. One caveat: equipment settings need adjustment as feed composition changes; a fixed setup can quietly increase losses.

What Are the Top Types of Glass Sorting Machines? — Mechanical Systems for the Initial Separation of Glass
Machine Type How It Separates Material Typical Separation Task Best Used For Key Considerations
Vibrating Screen A vibrating deck moves material across one or more screen surfaces; particles are separated according to whether they pass through the openings. Separating glass by particle size and removing small fines or oversized pieces. Early size classification of crushed glass or mixed incoming material. Screen openings determine the size split. Wet, sticky, or irregular material can reduce screening efficiency.
Rotary Trommel Screen A rotating perforated drum tumbles material, allowing smaller pieces to pass through its openings while larger pieces continue to the discharge end. Separating fine material from larger glass fragments and other bulky items. High-volume, relatively robust screening of mixed or irregular feed. Drum speed, angle, and aperture size affect separation. It classifies by size, not by glass color or material composition.
Ballistic Separator Inclined moving paddles or decks separate material according to its size, shape, and motion: rolling or rigid items move differently from flat or flexible items. Separating rolling containers and rigid objects from flatter packaging materials. Mixed packaging streams that contain glass containers alongside paper, film, and other materials. Performance depends on feed consistency and material condition. It is a physical separator, not a glass-color sorter.
Air Classifier Controlled airflow separates lighter materials from heavier pieces according to their aerodynamic behavior. Removing lightweight paper, labels, film, and other light contaminants from heavier glass. Dry processing lines where light contaminants need to be removed before further glass cleaning. Air settings and feed rate must be adjusted to limit glass loss. Dust control is important.
Magnetic Separator A permanent magnet or electromagnet attracts ferrous metals as material passes by or beneath the magnetic field. Removing iron and steel items, such as caps or fragments, from a glass stream. Metal removal before or after size reduction to protect downstream equipment and improve material quality. It removes magnetic metals; it does not separate glass from other nonmagnetic materials.
Eddy Current Separator A rapidly changing magnetic field induces currents in conductive nonferrous metals, causing them to be displaced from the main material flow. Recovering or removing nonferrous metals, such as aluminum, from mixed material. Processing streams that contain nonferrous metal alongside glass and other recyclables. It targets conductive nonferrous metals, not glass itself. Feed preparation and particle size influence performance.
Optical Glass Sorter Cameras or other optical sensors identify differences in color or material appearance; controlled air jets eject selected pieces. Separating glass by color or rejecting visible contaminants such as ceramics, stones, and heat-resistant glass. Later-stage cleaning when a more consistent glass cullet stream is required. It is a sensor-based sorting system rather than a purely mechanical separator. Results depend on presentation, cleanliness, and calibration.
Process note: A typical line combines several methods. Screens and trommels classify by size; air and ballistic separators handle differences in weight, shape, or motion; magnetic and eddy current units remove metals; optical sorters can perform more selective color and contaminant sorting.

Color Sorters for Separating Clear, Green, and Amber Glass

Color sorters separate clear, green, and amber glass by reading each piece as it moves along a conveyor. A controlled light source helps sensors detect differences in reflected or transmitted light. The system compares those readings with selected color thresholds, then uses timed air jets to divert unwanted pieces. Clear glass can appear cloudy when dust or labels remain. Green and amber fragments may also overlap in shade, especially under uneven lighting.

Consistent feeding matters. A deep, crowded layer can hide fragments from the sensors, while a thin, even spread gives each piece a clearer view. Operators typically check the belt, lighting, and air pressure during setup, then test the output by hand. Small adjustments can improve separation, but settings that work for one batch may not suit another. That matters. Broken edges, moisture, and mixed colors can confuse detection, so color sorting is not perfect on its own. A practical line may use screens or manual inspection before sorting to remove oversized pieces and obvious contaminants. It is worth measuring the reject stream, too; a machine can remove unwanted colors while accidentally sending usable glass aside.

Optical and Near-Infrared Sorters for Identifying Glass Types

Optical and near-infrared (NIR) sorters help processors separate glass by colour and material characteristics. Cameras capture visible colour, while NIR sensors read reflected light patterns to distinguish material classes. On a conveyor, this may mean separating clear, green, and amber fragments before an air jet knocks selected pieces into separate chutes. Small differences matter. Ceramic, stone, and porcelain fragments can resemble glass in colour, yet contaminate a recycled-glass batch.

The European Container Glass Federation reported an 80.1% glass-packaging recycling rate across the EU in 2022. The U.S. EPA’s 2018 materials report recorded a 31.3% recycling rate for glass containers. These figures reflect different regions and years, so they are not direct comparisons; they do show why accurate sorting remains important. In practice, sensor results depend on fragment size, surface dirt, moisture, and conveyor speed. NIR readings can also be less reliable on dark, coated, or mixed pieces, so operators often pair sensors with visual inspection and routine sample checks. No sensor is perfect. A useful setup is one calibrated against the actual incoming glass stream, then checked when feed conditions change.

What Are the Top Types of Glass Sorting Machines?

Optical and near-infrared sorters use different parts of the light spectrum to help identify materials.

Visible-light optical sorters can distinguish glass by color and appearance. Near-infrared (NIR) systems analyze spectral signatures; their effectiveness for glass depends on the material, feed conditions, and system design. The ranges shown are general spectral-region definitions, not guaranteed operating specifications for every machine.

X-Ray Sorters for Removing Ceramics, Stones, and Metals

X-Ray Sorters for Removing Ceramics, Stones, and Metals

X-ray sorters help separate unwanted materials that can look much like glass on a conveyor. Their sensors measure how X-rays pass through each piece, revealing differences in density and material composition. A pale ceramic chip may resemble clear glass to a camera, yet absorb X-rays differently. Stones and metal fragments can also trigger removal signals, depending on their size, position, and the machine’s settings.

Even good detection depends on a steady feed. When glass piles up or pieces overlap, contaminants may be hidden from the sensor. A well-adjusted system spreads fragments into a thin layer, scans them, and uses timed air jets to divert identified pieces into a reject bin.

Small pieces matter.

Operators should check test samples regularly and tune thresholds for the actual glass mix, rather than rely on one setting for every load. Too sensitive, and good glass may be rejected; too relaxed, and some contaminants can pass through. No setting is perfect. Reviewing reject material and final product samples helps reveal those trade-offs and keeps sorting decisions grounded in what the line is really processing.

AI-Enabled Multisensor Sorters for Complex Glass Streams

Glass streams are rarely uniform. A recycling line may receive clear bottles, green fragments, ceramic pieces, labels, and moisture together. AI-enabled multisensor sorters combine cameras, near-infrared sensing, and color or shape data. This helps identify pieces that one sensor alone might miss. The system can trigger air jets to separate target glass from unwanted material. Results depend on steady lighting, even belt loading, and regular calibration. Small, dusty fragments remain difficult.

These machines are most useful when glass types and contaminants vary across incoming loads. Before installation, operators should test representative samples and check whether the sorter meets their purity and recovery targets. Sensor settings may need adjustment as feed conditions change. AI can improve recognition, but it does not make every decision correct. A misread fragment can still enter the wrong stream, so periodic audits matter. That part is easy to underestimate.

Tips: Keep the belt evenly loaded. Clean sensors often. Review rejects by material type, and adjust settings when the feed changes.

Our story

When The Light Went On

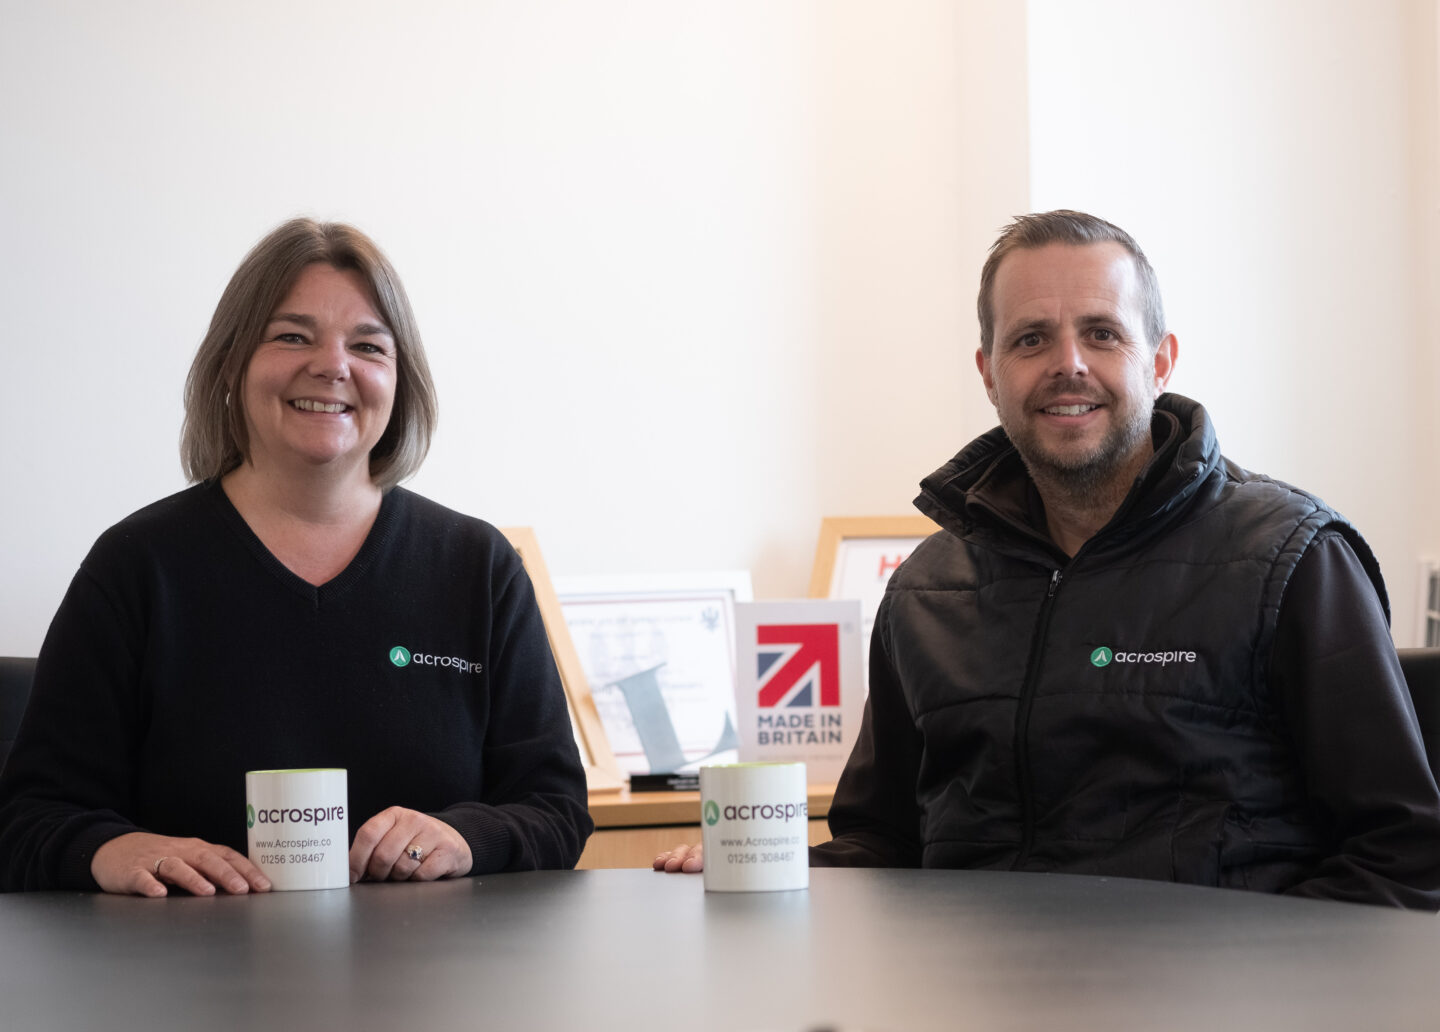
The idea for Acrospire was formed in 2012 when founder Tim envisioned a different kind of lighting manufacturer: one that would not only deliver outstanding customer experiences but also prioritise fair treatment for its employees.

We’ve come a long way

Working from any nook and cranny we could find

Motivated by the belief the industry wanted and needed better, Tim shared his plan to establish his own venture with Hatty, who simply couldn't let him do it alone.

The rest, as they say, is history.

Protecting local jobs and ensuring the best quality possible.

The products sold should, where possible be manufactured here in the UK

Working from a rented office by day and assembling lanterns in a garage at night, Tim and Hatty set to work.

11 Years later

and a lot has changed

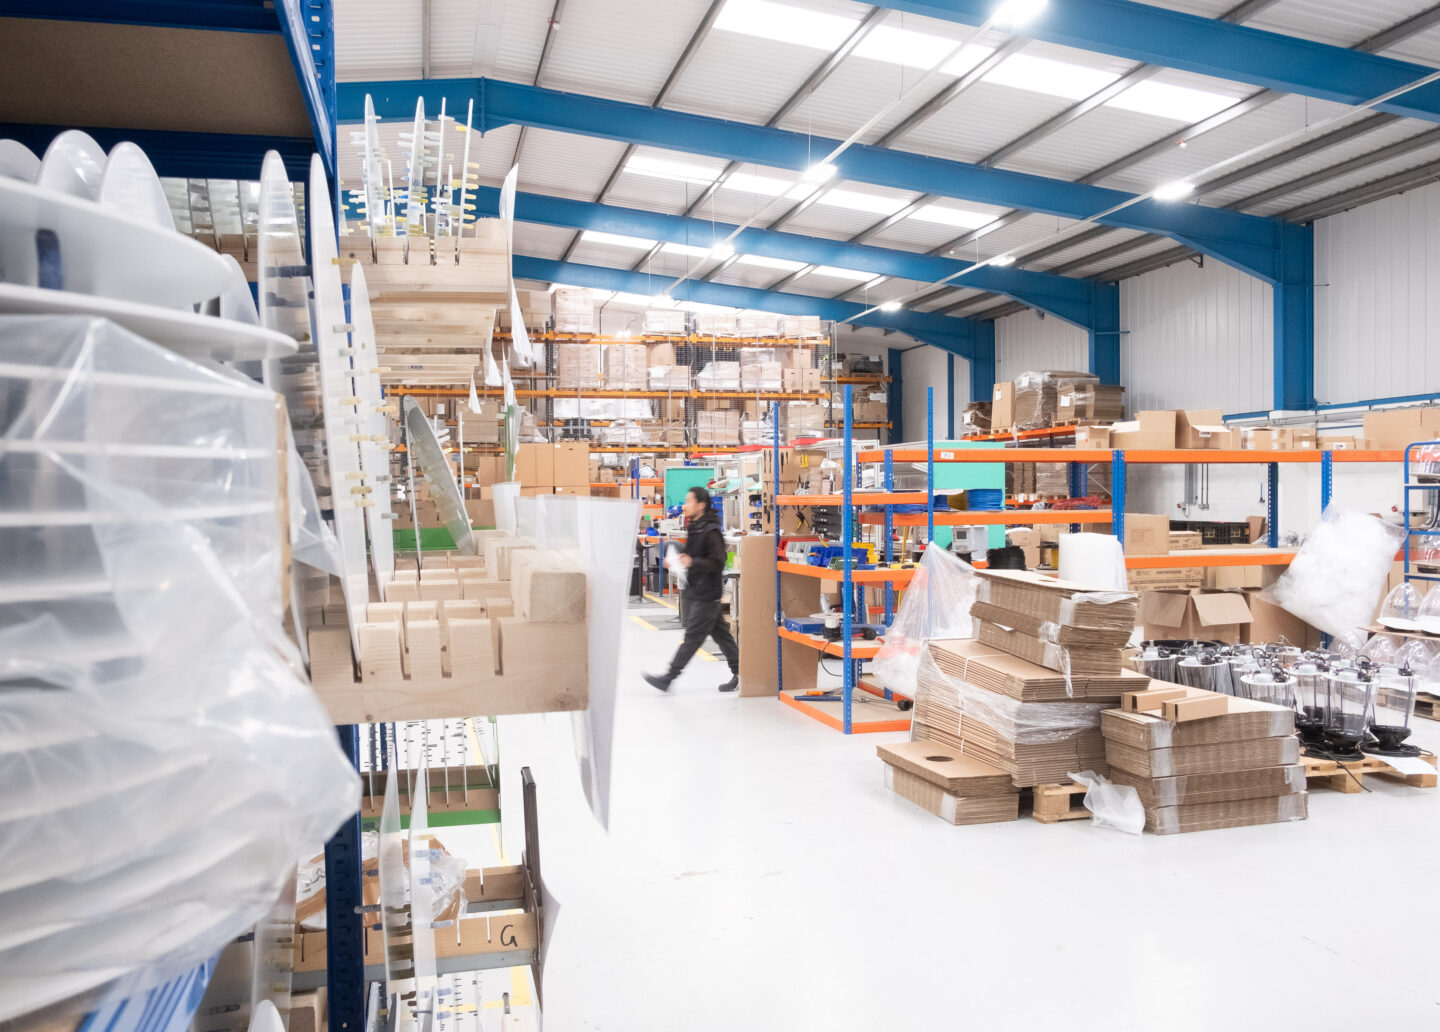
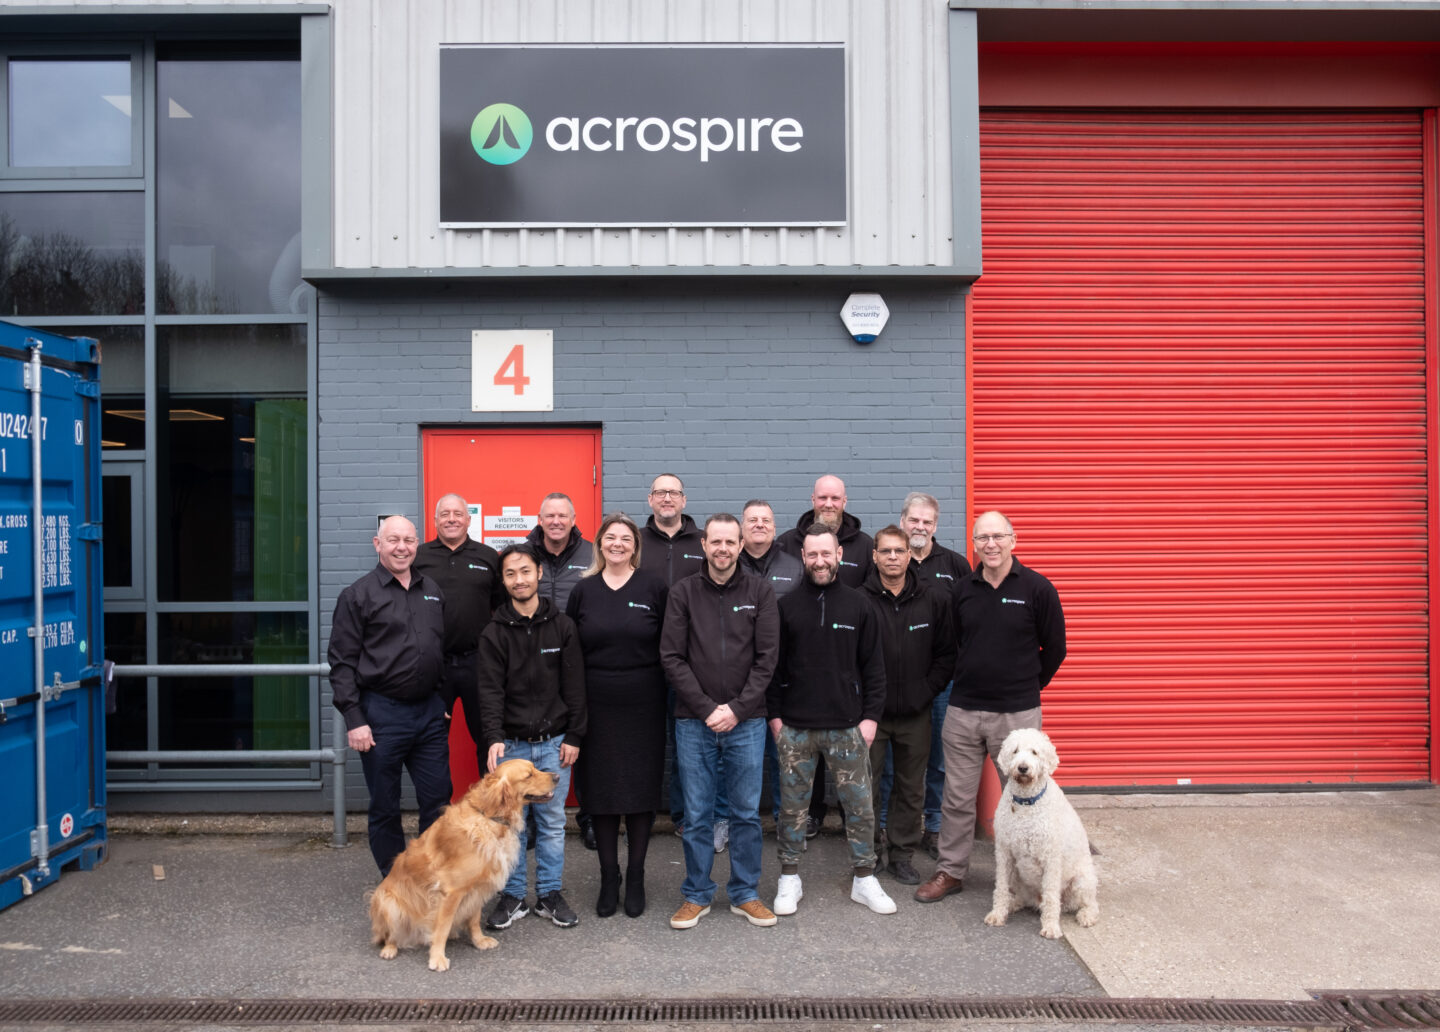
Acrospire now inhabits a 14000² ft manufacturing facility in Basingstoke, Hampshire. We’re a proud partner of the Made in Britain scheme, ISO9001 certified and a member of all relevant lighting industry trade bodies.

We've built a reputation to be proud of

Along with great relationships with our customers and a great team! We've attracted some of the most experienced members of the lighting industry, all by following one golden rule.

A simple ethos

Creating work to be proud of

That runs through all that we do. Customers who have made the switch to Acrospire have found working with us to be a breath of fresh air.

Market leading warranty

If you’re a professional in the lighting industry, you’re probably familiar with warranties that range from 3 to 10 years, with extensions available on special request or at additional cost. At Acrospire, where we’re proud to be different, we offer a market-leading simple 12-year warranty, as standard.

Tight Control on Quality

We focus on our customers not our competition. We manufacture our products in the UK: with the exception of our solar products, our supply chain is within a 60-mile radius of our factory in Basingstoke: to maintain greater control over quality. We al

Speed is key

Speed of response is crucial when it comes to resolving warranty issues. If we’ve made a mistake, we own it, get to the root cause, and fix it as quickly as possible. We believe in timely communication with our customers and making the resolution pro

Test and Test Again

We believe in independent testing and certification. Our new product development is in line with ISO 9001. Many of our products hold ENEC Certification. To meet the requirements of ENEC we also send random product samples for third party safety testi

Quality by design

Our product design is another key factor in our ability to offer a 12-year warranty. We value engineer rather than cost cut, never compromising on quality. We stick to our processes and engage with our supply chain to ensure that every product meets