shining bright

a British lighting manufacturer with a difference

Obsessed with solving problems, not just selling 'stuff': we were born from a belief that the lighting industry deserved better.

7 Tips for Choosing a New Energy Car Production Line

A New Energy Car Production Line is a major investment, shaping product quality, output, and operating costs for years. Choosing one involves more than comparing machines or accepting the fastest production estimate. Battery formats, vehicle designs, automation levels, and factory space all affect how well equipment works together. A line built for today’s model may need costly changes when the next platform arrives.

Details matter. Consider a battery-pack station: its handling equipment, torque tools, and inspection systems must suit the pack’s dimensions and process requirements. Ask suppliers how they validate cycle times, track defects, and support commissioning—not just what their brochures promise. Check whether proposed capacity accounts for changeovers, maintenance, and operator training. These practical questions can reveal gaps early. They also make supplier claims easier to evaluate.

No two projects have identical priorities. A startup may value flexible tooling, while an established manufacturer may need stable, high-volume output. Forecasts can be wrong, and even careful plans deserve review. That is not a reason to avoid investment; it is a reason to test assumptions against realistic demand and production data. This guide outlines seven tips for comparing line capacity, process compatibility, automation, quality controls, utilities, supplier support, and total cost of ownership. The aim is a decision grounded in measurable needs, not impressive specifications alone. A little doubt helps. Better questions often lead to a more reliable line.
7 Tips for Choosing a New Energy Car Production Line

Understanding the Scope of a New Energy Car Production Line

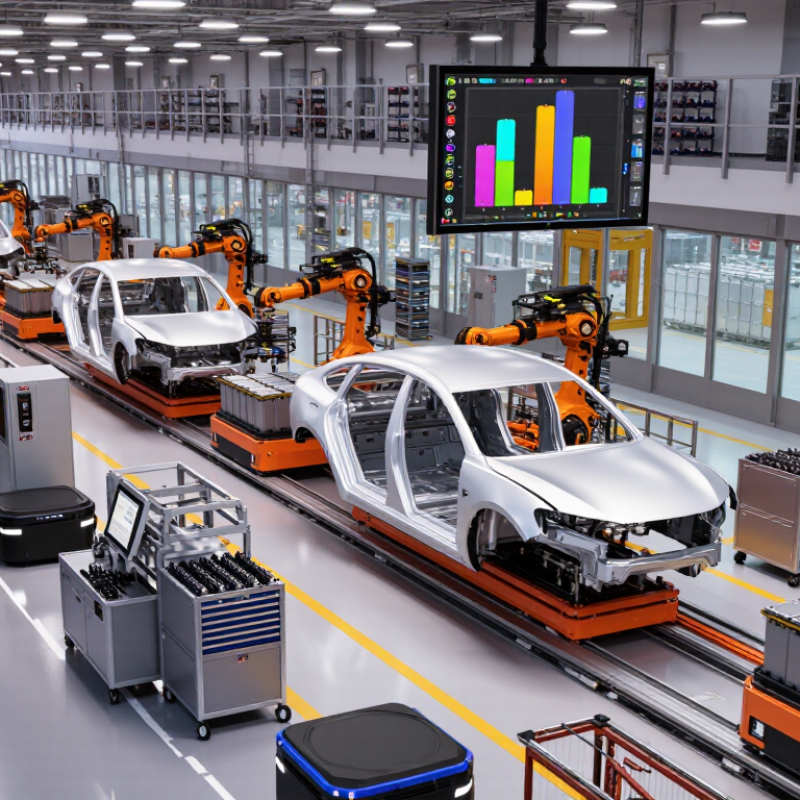
A new energy car production line is more than a row of machines. Its scope covers the full route from incoming materials to a tested vehicle.

Depending on the vehicle design, that route may include body fabrication, coating, battery-pack assembly, electrical integration, and final inspection. Scope matters. A battery area, for example, needs defined material flows, controlled work conditions, equipment access, and safe handling procedures. These details affect building layout and utility planning, not just the equipment budget.

Define the planned vehicle types, output rate, shift pattern, and degree of automation before comparing line proposals. Then map each operation and its handoffs. Where does the battery pack enter the process? How are software checks, leak tests, and end-of-line inspections recorded? Traceability should connect results to each vehicle without slowing routine work.

A spreadsheet can hide awkward gaps between stations. This estimate is rarely neat. Teams should also identify what falls outside the line supplier’s scope, such as facility upgrades, workforce training, or integration with existing systems. Those boundaries are easy to overlook, and they can change both the schedule and the real cost. A phased plan may help, but only if future capacity and floor space are considered early.
Assessing Production Goals, Vehicle Types, and Capacity

7 Tips for Choosing a New Energy Car Production Line

Assessing Production Goals, Vehicle Types, and Capacity

Before comparing production lines, define what the factory must build each day. Set targets for annual output, shift patterns, and planned growth. Then list the vehicle types and expected model mix. A line designed for one vehicle configuration may struggle when battery sizes, body styles, or assembly steps vary. Check how the layout handles those changes. A few minutes lost at each changeover can affect daily output.

Tip: Map each major process, from body assembly to final testing. Note where battery packs, motors, and vehicle bodies arrive, and how workers or automated systems move them. Compare the required cycle time with realistic operating hours. Leave room. Include maintenance, staff breaks, and model changeovers in capacity estimates.

Ask suppliers for clear assumptions behind their quoted output. Confirm whether figures include inspections, rework, and routine stops. A short site visit or process simulation can reveal bottlenecks near paint, battery installation, or end-of-line testing. These details matter. One forecast will probably be wrong; revisit it as orders and product plans change. Avoid choosing a line that only meets targets under perfect conditions.

7 Tips for Choosing a New Energy Car Production Line

Assessing Production Goals, Vehicle Types, and Capacity

This illustrative planning scenario compares annual production goals with planned effective line capacity. Values are hypothetical, in thousands of vehicles per year, and are not industry benchmarks. Use your forecast, vehicle mix, shift schedule, and expected line efficiency to set actual capacity requirements.

Comparing Automation, Equipment, and Battery Assembly Needs

7 Tips for Choosing a New Energy Car Production Line

A production line should match the vehicle design, expected output, and available floor space. High automation can improve repeatability, but only when product designs and process steps remain stable. For flexible models, modular stations and adjustable fixtures may be more useful than a fully dedicated line. Fit matters more. Compare cycle time with changeover time, maintenance access, and operator training needs—not just the headline capacity.

Battery assembly deserves separate scrutiny. The International Energy Agency’s Global EV Outlook 2024 reports that electric-vehicle battery demand reached about 750 GWh in 2023, a 40% increase from 2022. That growth makes scalable equipment important, but it does not mean every factory needs maximum automation. Check cell-handling precision, traceability, in-line inspection, and safe storage conditions. Ask suppliers to demonstrate how the equipment handles real cells and tolerances. Not just speed.

Equipment choices should reflect the battery format and pack architecture. A line may need cell stacking or module assembly, laser joining, sealing, electrical testing, and end-of-line validation. Confirm that data systems can link each pack to its process records. The awkward part: integration often takes longer than the equipment installation. Build time for commissioning and process tuning into the plan, and request measured test results before accepting promised throughput.

Evaluating Suppliers, Costs, Safety, and Quality Standards

A production line should fit the vehicle mix you expect to build, not just the capacity shown in a sales presentation. The International Energy Agency’s Global EV Outlook 2024 reports nearly 14 million electric-car sales in 2023, about 18% of global car sales. That growth supports scalable equipment, but forecasts vary by market. Ask suppliers to demonstrate model changeovers, cycle-time performance, and operator training on equipment similar to yours. Small details matter.

Compare total ownership costs, not only the purchase price. Include tooling, utilities, maintenance, software, spare parts, and planned downtime. BloombergNEF reported average lithium-ion battery-pack prices of $139 per kilowatt-hour in 2023, down 14% from 2022. This is not a production-line cost, but it shows why battery and process assumptions should be stress-tested. No quote tells the whole story.

Safety and quality need observable evidence. Review risk assessments against ISO 12100, and verify safety-control functions against applicable ISO 13849 requirements. Ask to see interlock tests, emergency-stop records, and procedures for handling battery modules. For quality, check how the line traces each component and records torque, weld, or leak-test results. Request sample data, not promises. A polished demonstration can still hide difficult maintenance access or inconsistent changeovers; leave time for an independent review before acceptance.

7 Tips for Choosing a New Energy Car Production Line — Evaluating Suppliers, Costs, Safety, and Quality Standards
Tip Evaluation Area What to Assess Practical Data or Check Evidence to Request
1. Define the production requirement Capacity and product flexibility Confirm vehicle variants, planned shifts, process sequence, staffing assumptions, and required annual output before comparing proposals. Calculate required cycle time as available production time divided by required units. State the planned operating calendar and whether the quoted capacity is theoretical or demonstrated. Process flow, cycle-time study, line-balance analysis, capacity assumptions, and a list of included vehicle variants.
2. Verify supplier capability Relevant experience and delivery support Check experience with comparable processes, such as body assembly, paint, final assembly, battery-pack handling, or end-of-line testing. Assess local service coverage and spare-parts support. Compare project scope, commissioning responsibilities, response arrangements, training, and warranty terms—not just the supplier’s claimed line capacity. Reference-project details, project schedule, service and escalation plan, training plan, warranty scope, and spare-parts list.
3. Compare total cost of ownership Capital and operating costs Include equipment, installation, utilities, software, tooling, integration, building modifications, training, maintenance, and planned upgrades. Compare costs over the same evaluation period and production assumptions. Include energy use, consumables, labor, maintenance, and expected downtime in operating-cost estimates. Itemized quotation, exclusions and assumptions, utility-load list, maintenance schedule, consumables list, and lifecycle-cost calculation.
4. Make safety a design requirement Machine and battery-process safety Review guarding, interlocks, emergency stops, safe access, robot-cell protection, electrical isolation, lifting operations, and controls for battery-related hazards. Require a documented risk assessment and hazard controls appropriate to the equipment and site. Check applicable regulations and standards, including ISO 12100 for machinery risk assessment and ISO 13849-1 for safety-related control systems. Risk assessment, safety circuit documentation, safeguarding layout, lockout procedures, validation records, and operator training materials.
5. Set measurable quality criteria Process control and traceability Assess inspection methods, error-proofing, calibration, defect handling, process records, and traceability for components and production steps. Define acceptance criteria for each process and product test before contract award. Use the OEE formula—availability × performance × quality—when comparing operational performance, and agree how each input is measured. Quality plan, inspection and test plan, traceability example, calibration records, defect-escalation process, and agreed performance definitions.
6. Check compliance and system integration Standards, controls, and interfaces Confirm machinery, electrical systems, software, and factory interfaces meet the rules applicable at the installation site and work with the plant’s existing systems. Review relevant requirements such as IEC 60204-1 for electrical equipment of machines and ISO 9001 for quality management systems. Apply automotive-sector requirements only where relevant to the organization and contract. Compliance matrix, electrical schematics, interface specifications, software and data-access provisions, and applicable management-system certificates.
7. Prove performance before acceptance Testing, commissioning, and handover Agree how equipment will be tested at the supplier’s facility and at the production site, including output, quality, safety, changeover, and recovery from faults. Set pass/fail thresholds, test duration, product mix, operating conditions, and remedies in the contract. Do not rely on an output figure unless its measurement conditions are defined. Factory and site acceptance test protocols, commissioning plan, punch-list process, training sign-off, final documentation, and performance-test results.

Planning Installation, Workforce Training, and Future Expansion

A new energy car production line needs more than floor space and equipment. Installation planning should begin with a measured site layout, including column positions, utility routes, material paths, and maintenance access. Check power capacity, ventilation, compressed air, and charging needs before equipment arrives. A missed cable trench can delay commissioning. Allow room for safe vehicle movement and future service work, not just the machines themselves. Even a careful plan can overlook awkward corners; a walk-through with operators may reveal them.

Tip: Mark the proposed line on the floor with tape. Move sample parts along the route, and note where carts, people, or lift equipment might cross.

Workforce training should match each station and its real tasks. Use hands-on practice for battery handling, torque checks, inspection steps, and emergency procedures. Give new operators time to repeat tasks with a trainer nearby. Short checklists help, but they cannot replace good coaching. Some training plans look complete on paper and still leave workers unsure about a small changeover.

Plan future expansion around likely needs, not optimistic guesses. Reserve space for another station, extra testing capacity, or a wider material lane. Keep utility connections accessible and document equipment settings. Review expansion assumptions as product designs and production volumes change. Space has a cost, of course. A phased plan may be more practical than building for every possibility at once.

Our story

When The Light Went On

The idea for Acrospire was formed in 2012 when founder Tim envisioned a different kind of lighting manufacturer: one that would not only deliver outstanding customer experiences but also prioritise fair treatment for its employees.

We’ve come a long way

Working from any nook and cranny we could find

Motivated by the belief the industry wanted and needed better, Tim shared his plan to establish his own venture with Hatty, who simply couldn't let him do it alone.

The rest, as they say, is history.

Protecting local jobs and ensuring the best quality possible.

The products sold should, where possible be manufactured here in the UK

Working from a rented office by day and assembling lanterns in a garage at night, Tim and Hatty set to work.

11 Years later

and a lot has changed

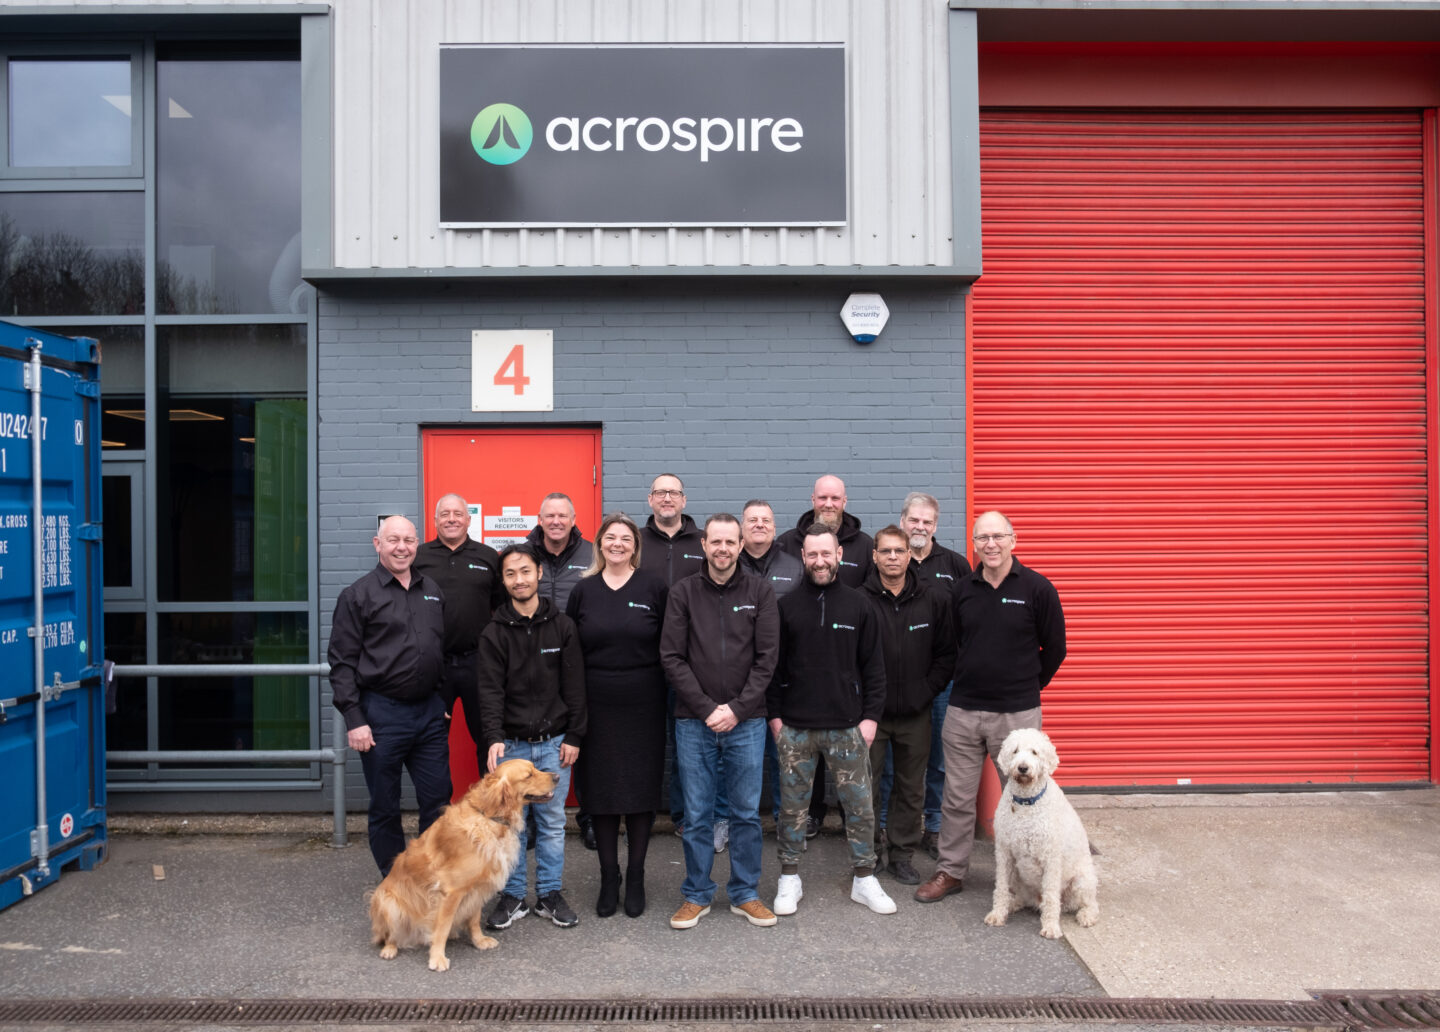
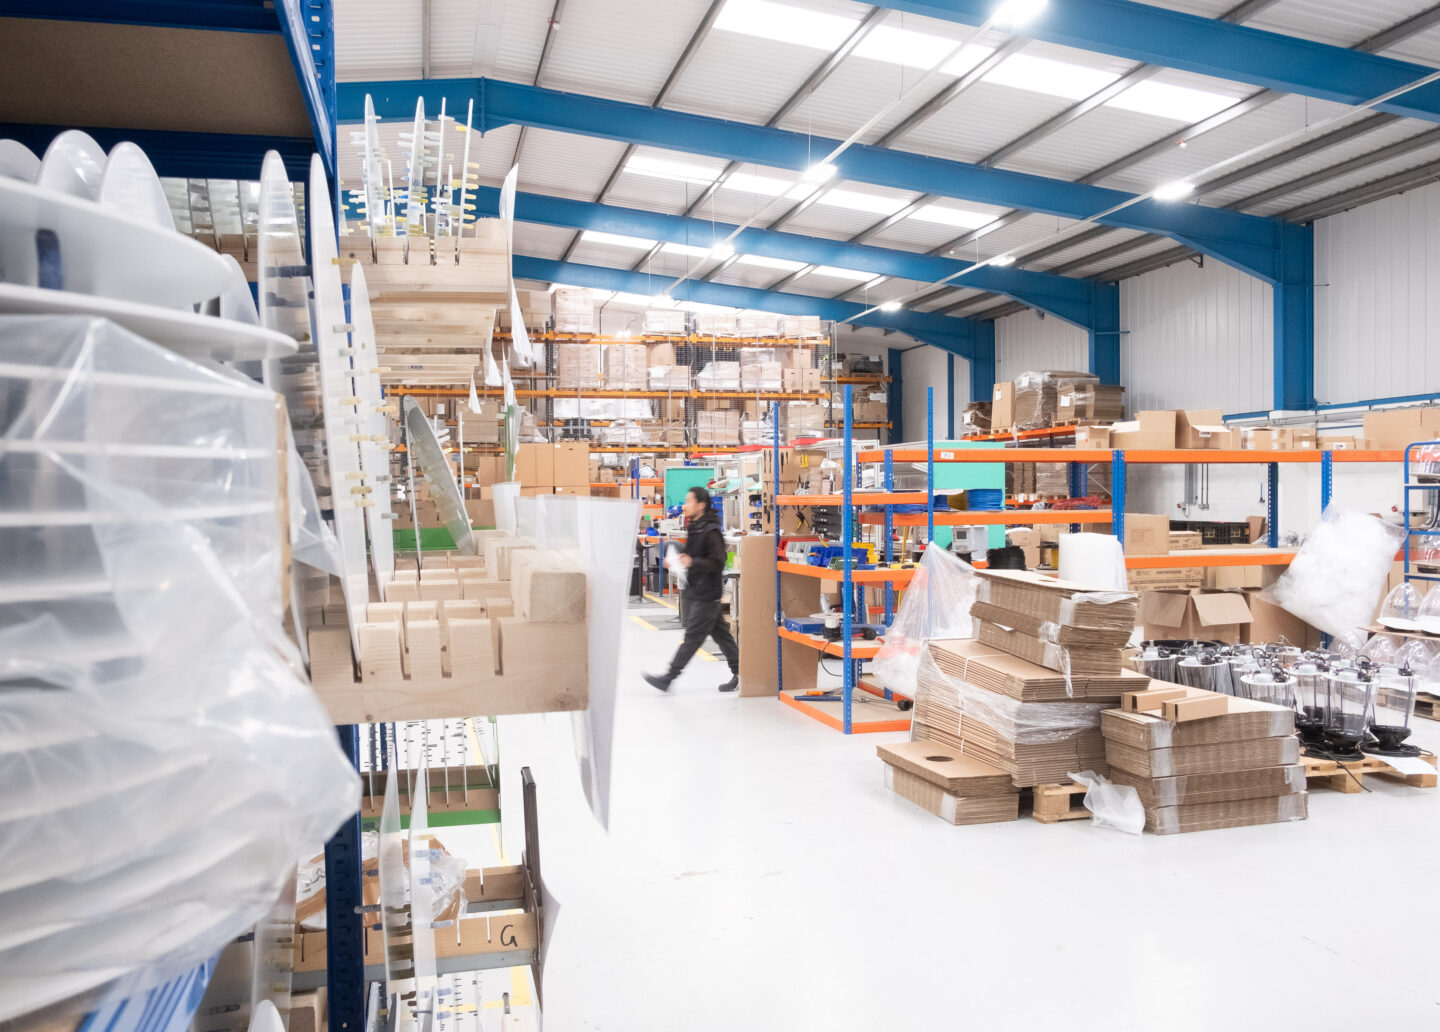
Acrospire now inhabits a 14000² ft manufacturing facility in Basingstoke, Hampshire. We’re a proud partner of the Made in Britain scheme, ISO9001 certified and a member of all relevant lighting industry trade bodies.

We've built a reputation to be proud of

Along with great relationships with our customers and a great team! We've attracted some of the most experienced members of the lighting industry, all by following one golden rule.

A simple ethos

Creating work to be proud of

That runs through all that we do. Customers who have made the switch to Acrospire have found working with us to be a breath of fresh air.

Market leading warranty

If you’re a professional in the lighting industry, you’re probably familiar with warranties that range from 3 to 10 years, with extensions available on special request or at additional cost. At Acrospire, where we’re proud to be different, we offer a market-leading simple 12-year warranty, as standard.

Tight Control on Quality

We focus on our customers not our competition. We manufacture our products in the UK: with the exception of our solar products, our supply chain is within a 60-mile radius of our factory in Basingstoke: to maintain greater control over quality. We al

Speed is key

Speed of response is crucial when it comes to resolving warranty issues. If we’ve made a mistake, we own it, get to the root cause, and fix it as quickly as possible. We believe in timely communication with our customers and making the resolution pro

Test and Test Again

We believe in independent testing and certification. Our new product development is in line with ISO 9001. Many of our products hold ENEC Certification. To meet the requirements of ENEC we also send random product samples for third party safety testi

Quality by design

Our product design is another key factor in our ability to offer a 12-year warranty. We value engineer rather than cost cut, never compromising on quality. We stick to our processes and engage with our supply chain to ensure that every product meets